

- Home
- >
- Products
- >
- Manifold Casting
- >
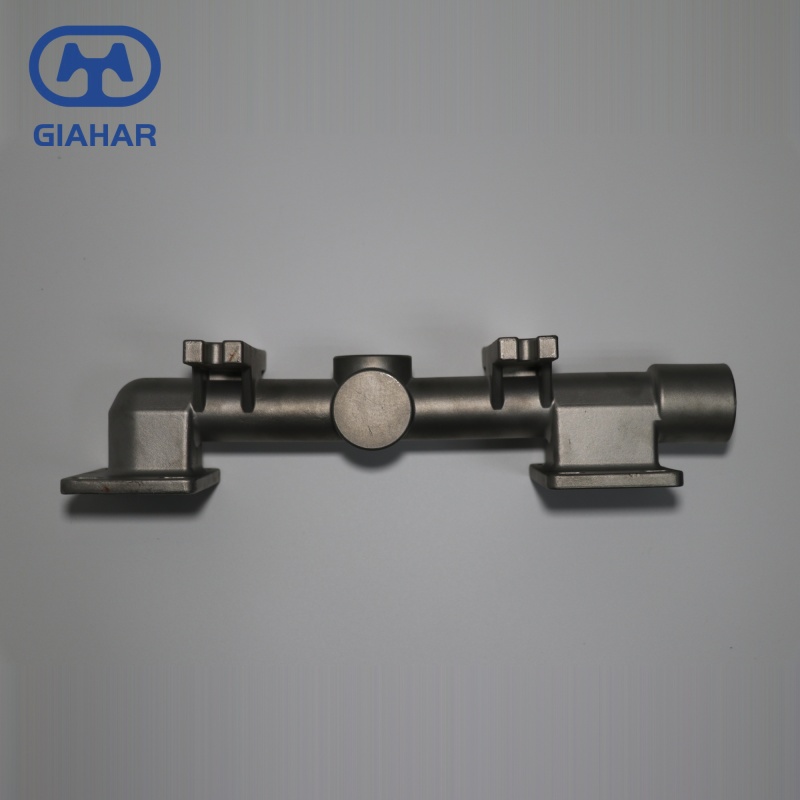
Manifold Casting
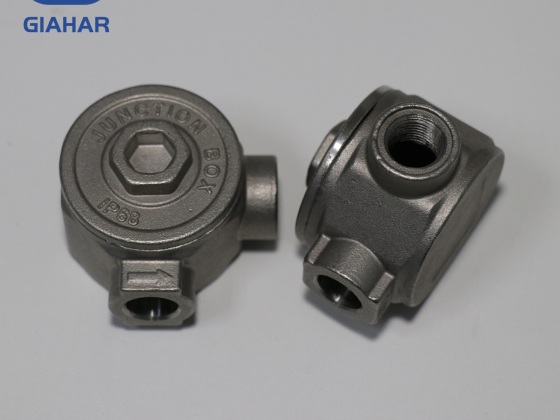
• 304 and 316L manifold castings for hydraulic, chemical and water systems
• Silica sol investment casting with in-house CNC machining of ports and sealing faces
• Port positions and sealing faces machined to ±0.05 mm
• Custom port layouts reviewed at DFM to reduce machining time and casting scrap
- China
- New product development: 2 months; precision casting production: 1.5 months; schedule can be adjusted according to production conditions.
- 1,000 tons per year (precision casting)
- Information
Stainless Steel Manifold Casting
Most manifold problems show up at a drilled crossing, not on the outside. Two channels pass close together, and the wall between them can be thin. Boring ports a small fraction too shallow can cause the valve assembly to be off angle. Our valves have 304 or 316L cast bodies, they are stressrelieved and we are the ones machining the ports and sealing faces for the bodies in our own workshop.
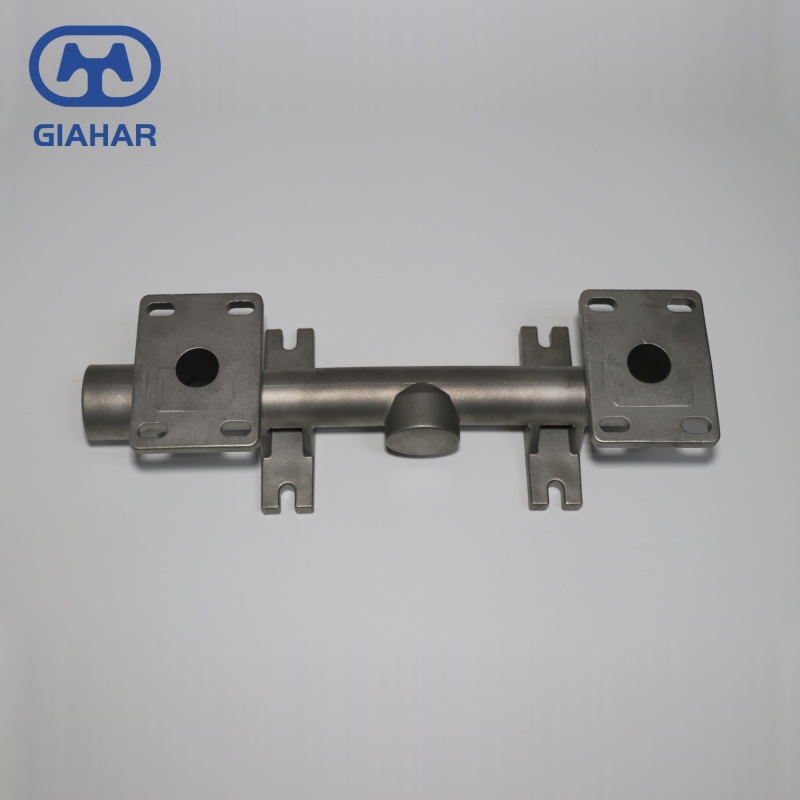
The table below gives the normal working range for this manifold. Final dimensions, port layout and inspection level are confirmed from the drawing.
| Material | 304 or 316L stainless steel; 316L for corrosive duty |
| Casting process | Silica sol investment casting, poured in our own foundry |
| Casting weight | 0.5–30 kg; envelope up to 400 mm, depending on drawing |
| Machining tolerance | ±0.05 mm on port faces and bore; ±0.10 mm on general features |
| Surface roughness | Ra 1.6–3.2 µm on sealing faces; Ra 6.3–12.5 µm as-cast |
| Pressure and temperature | PN10–PN40 / Class 150–300; -20 °C to 200 °C, subject to design and gasket |
| Ports and connections | Threaded, flanged or custom port layout machined to drawing |
| Heat treatment | Stress relief after casting; solution annealing on request |
| Inspection | Dimensional report and visual inspection |
| Finish and packing | Finish: As-cast, machined, passivated or pickled. Packaging: Machined faces get a rust-preventive film and extra wrapping. Parts are kept apart in the pack so they cannot hit each other. We use export cartons, fumigated or non-fumigated wooden cases, and EU-standard boxes or pallets. Other packing can be made to order. Environmental compliance: Packaging follows Regulation (EU) 2025/40 (PPWR), which applies in EU member states from 12 August 2026. |
Port spacing, thread type and branch position are machined to the customer drawing. Two manifolds can look alike outside and have different internal routing, so the price is quoted from the drawing and inspection requirements.
Why the Intersections Matter
Cross-drilled channels meet inside the body, often with only a limited wall between them. If the casting shifts during cooling, or the drill enters at an angle, the wall can become thin on one side. The leak does not appear until the manifold is under pressure. Valve mounting faces have the same problem: a face that is not flat will not seal, even with a good gasket.
We stress relieve the casting before machining and check port position, face flatness and thread depth against the drawing. The inspection is focused on the features that control sealing and assembly, not only the outside shape.
Casting and Stress Relief
This pattern is first made by injecting wax into a model, and then after several dippings with a ceramic coating to make the shell thick enough it's fired. 304 or 316L steel is poured in only once they've finished their firing step. The ceramic coating is put over the pattern in several layers. Drying each layer before going for the next one is important. Then the shell is fired. 304 or 316L is poured in the shell. Silica sol, in comparison, gives a better finish than sand. This is of help when channels are very closely running together. After shakeout the casting is submitted to a stress relief cycle. Otherwise the ports can shift during machining.
Thin sections between channels are reviewed at the DFM stage. If a port layout leaves too little metal between two passages, the design is adjusted before tooling rather than discovered at the drill.
Machining Ports and Sealing Faces
The castings go directly to our CNC shop. We face the mounting pads, bore the cross passages and cut the port threads to the drawing. Where the geometry allows, several features are machined in one setup so they stay related to each other. Firstly components are checked prior to serial production, and the process is under direct supervision of the machine operator who keeps a close eye on critical dimensions of the part during the whole run.
If a casting and machining operation is done at one factory it will be much easier to catch a wall-section or a port-position issue before the next batch is poured. It is also beneficial when adjustments to a sample part are necessary since the distance is reduced considerably.
Custom Manufacturing Process
1. Drawing Review
We start with the drawing, material grade, port layout, pressure rating and order quantity. Any packing or documentation requirement is recorded at this stage.
2. Feasibility Check
The engineering team reviews the wall between channels, machining access, fixture design and casting yield. Features that could cause leakage or tool breakage are raised before tooling.
3. Sample Approval
When a sample is required, a first part is produced and checked for port position, face flatness and thread depth. Production starts only after the sample is approved.
4. Batch Scheduling
Casting, machining and finishing are planned as one route. The batch is tracked against the approved specification and quantity.
5. Inspection and Records
Dimensional and visual checks are performed to the agreed requirements. The results stay with the batch for traceability.
6. Packing and Shipment
Machined faces are protected, the manifolds are packed for export, and the agreed labels and shipping documents are prepared.
Engineering Support and Cost Control
Port layout has a direct effect on cost. The price is not only the casting weight. It also depends on how the part is held, how far the drill travels and how many setups are needed. We review those points with the foundry and machine shop before tooling. If a port can move without affecting the function, or a clearance can be opened, we suggest it. The aim is to remove machining time, not to change the material or pressure rating.
Cost control comes from stable tooling, consistent wall sections and a machining sequence that matches the batch size. Lowering the material grade or skipping inspection would reduce the quote, but it would move the cost to the customer's assembly line.
Where It Goes
These manifolds are used in hydraulic power units, chemical dosing skids, water treatment systems, food and beverage lines, instrument panels and compressor packages. Most of our customers are in Japan, South Korea, Europe and North America. If the fluid is aggressive or the pressure cycles are high, the grade and wall section are reviewed before quotation.
A hydraulic manifold block is quoted from the same drawing as a stainless steel manifold.
Company Profile & FAQ
| At a Glance | |||
| Founded | 2010 | ||
| Factory Area | About 60,000 m² in Kazuo County, Liaoning, China | ||
| Staff | Around 120 people, including engineers and QC | ||
| Experience | 16 years of silica sol investment casting | ||
| Export Markets | Japan, South Korea, Europe and North America | ||
| Capacity | 1,000 tons per year of precision castings | ||
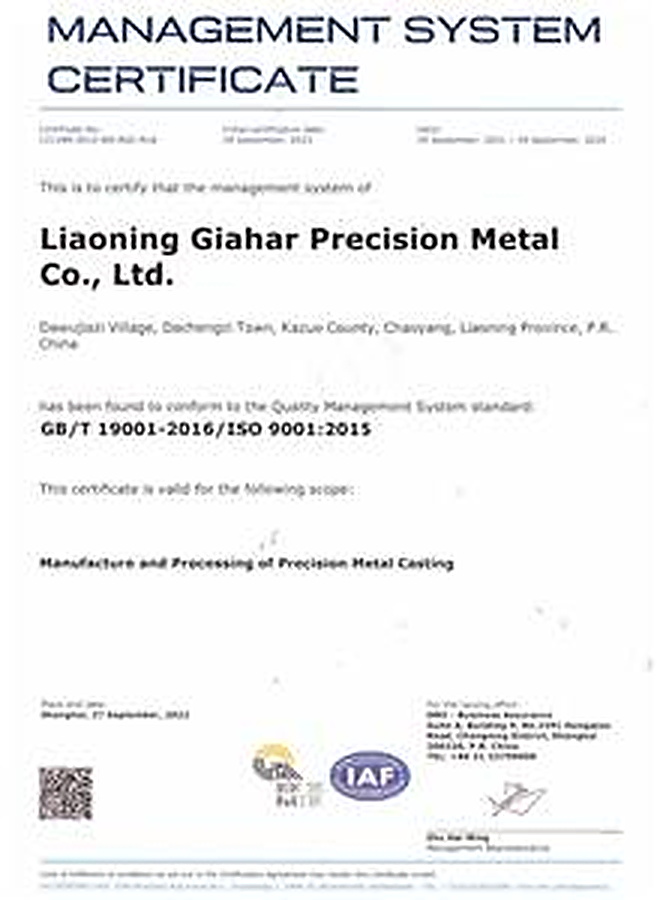
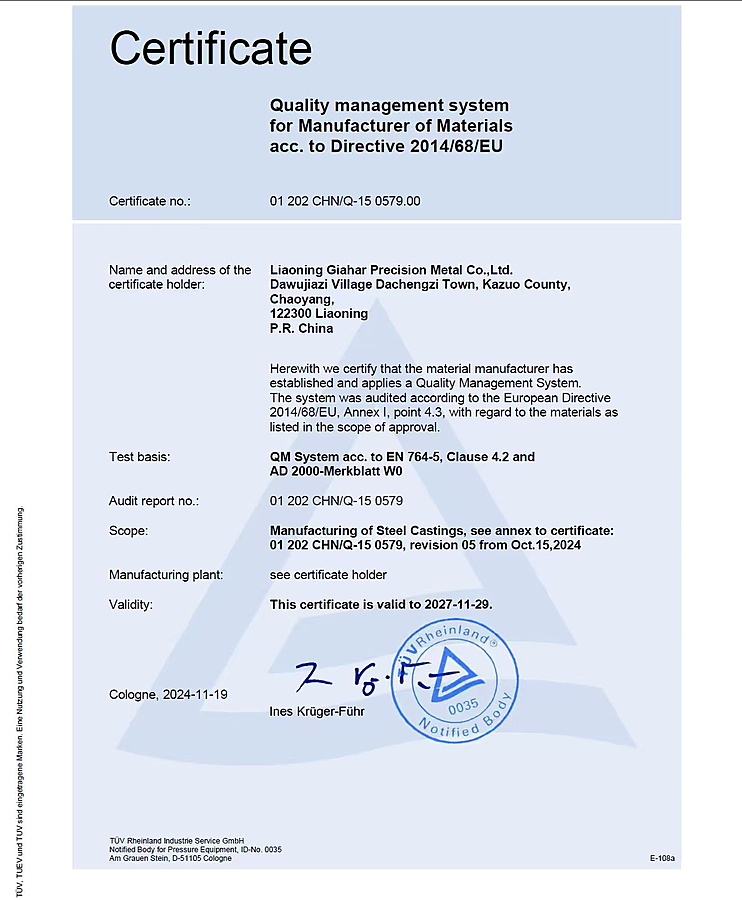
| Certifications | DNV ISO 9001 Quality Management System Certificate; TUV PED 2014/68/EU Pressure Equipment Certificate
| ||
| Common FAQ | |||
| Q: Can you produce parts from a drawing or sample? | |||
| Send the drawing, a 3D model or a sample. Before quoting, we check wall sections, port positions, machining stock and tolerances. Anything that looks difficult is raised before tooling. | |||
| Q: What certificates and reports can you provide? | |||
| We can supply mill certificates to EN 10204 3.1, heat treatment records and dimensional reports. PED 2014/68/EU documentation and a hazardous-substance-free declaration covering RoHS and REACH are available as well. The document package is agreed at quotation. | |||
| Q: Is machining, heat treatment and surface finishing done in house? | |||
| Yes. Castings go from our foundry to our CNC shop. Stress relief is done after casting, and solution annealing can be done in our controlled furnace when the specification calls for it. Passivation and pickling are also handled on site. | |||
| Q: Which standards do you work to? | |||
| European jobs usually follow ISO. Drawing calls for a standard other than ISO? Include it with the enquiry. We will check what the inspection needs before quoting, and agree the method before the order is released. | |||
| Q: What are the MOQ and lead times? | |||
| MOQ is normally 100–500 pcs for new tooling, with lower quantities for repeat orders. New product development takes about 2 months, and precision casting production takes about 1.5 months. The final schedule depends on the drawing, quantity and current production load. | |||
Manifold Casting FAQ
| Product-Specific FAQ | |
| Q: Can the cross-drilled passages and port threads be machined to my drawing? | |
| Yes. Port positions, cross passages and thread sizes are machined to the drawing. The fixture and machining sequence are reviewed before the first batch, and a first-off part is checked before serial production. | |
| Q: What is the typical wall thickness between internal channels? | |
| This is reviewed at the DFM stage because it depends on port size and pressure rating. Sometimes the drawing leaves very little metal between two passages. That is a risk at the drill and at the pressure test. If there is room, we add wall thickness between the channels. The casting distorts less, and the drill has a straighter path. | |
| Q: How do you control port position and face flatness? | |
| Port centre distance, face flatness and thread depth all get checked against the drawing. | |
| Q: Can you supply the manifold in 304 or 316L? | |
| 304 covers general service. 316L is the better choice for corrosive media or frequent cleaning. We confirm the grade from the fluid and temperature. | |
| Q: Can you help reduce the cost of the manifold? | |
| Yes. Port layout, wall sections, machining stock, fixture access and batch size all affect the price. A small change can shorten drilling, reduce tool wear or improve casting yield without changing the function. |