

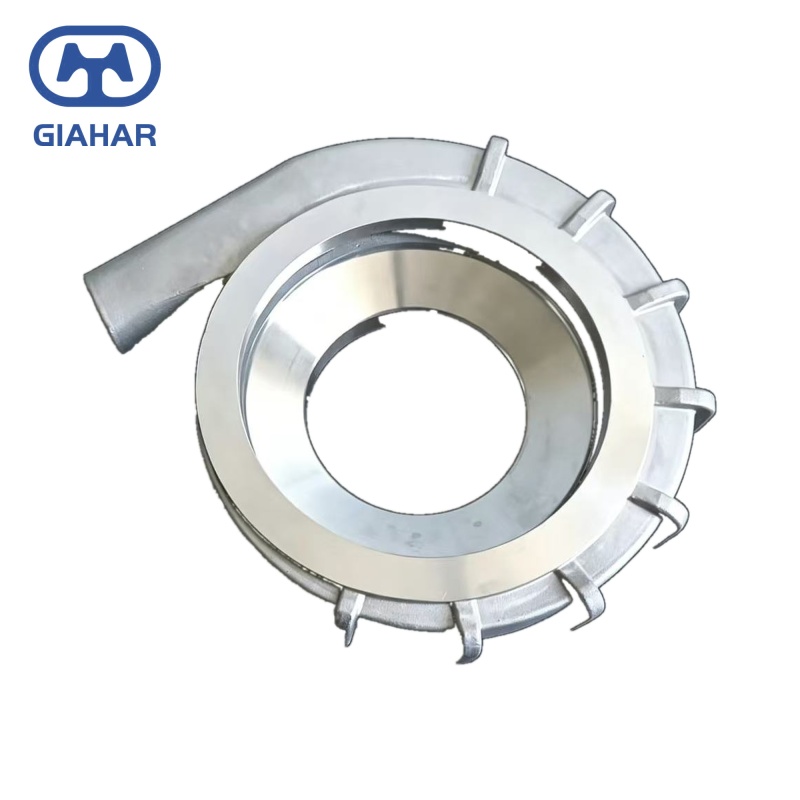
Pump Body Stainless steel 316L High sealing & pressure resistance
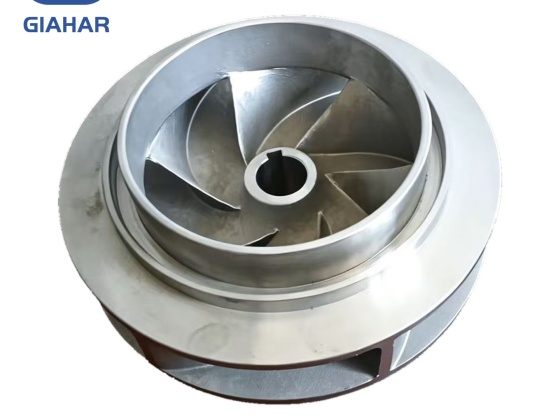
• 316L stainless steel pump body / volute casing for chemical and seawater service
• Silica sol investment casting, one-piece body with no welded seams
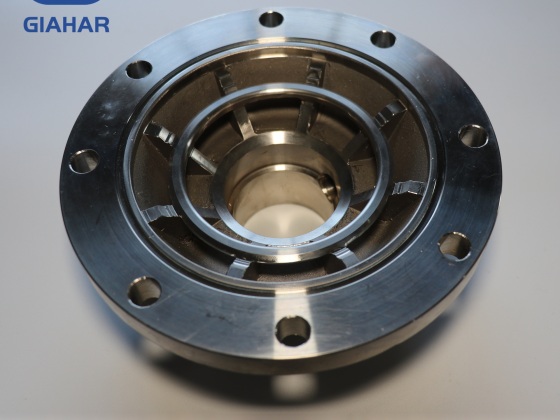
• CNC machined flanges, bore and seal seat
• Pressure tested before shipment
- China
- New product development: 2 months; precision casting production: 1.5 months; schedule can be adjusted according to production conditions.
- 1,000 tons per year (precision casting)
- Information
Stainless Steel Pump Body 316L
A pump body has to hold pressure, line up with your piping, and keep the seal faces flat for years. We investment cast these in 316L on our silica sol line and finish every flange, bore and seal seat on our own CNC stations. You get the machined casing direct from our foundry, no trader standing between the casting floor and your receiving dock. The body is a pressure boundary, and the pressure test is recorded before packing.
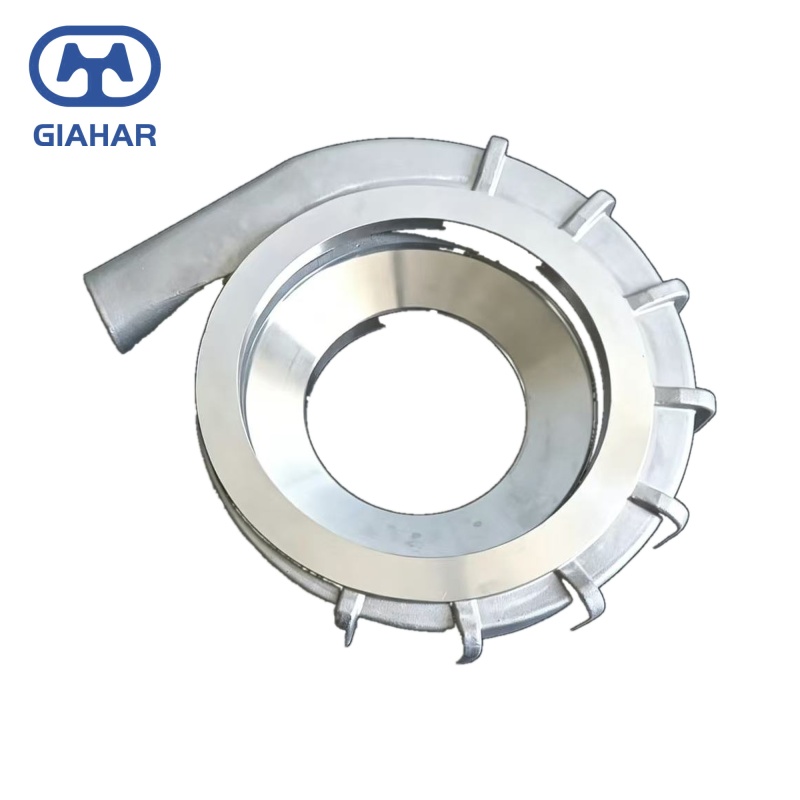
The table below gives the normal working range for this pump body. Final flange, bore and seal dimensions are confirmed from the drawing. Pressure tightness is checked before packing.
| Material | 316L stainless steel |
| Casting method | Silica sol investment casting, in our own foundry |
| Body type | Volute casing for centrifugal pump |
| Flanges and bore | CNC machined to drawing |
| Seal seat | Fine machined sealing face |
| Pressure test | Per drawing before shipment |
| Heat treatment | Stress relief; solution annealing on request |
| Inspection | Visual and dimensional check; material certificate |
| Finish and packing | Finish: As-cast, machined, passivated or pickled. Packaging: Anti-rust fluid on machined surfaces, with extra protection for machined faces and impact protection to prevent transit damage. Export carton, fumigated wooden crate, non-fumigated wooden crate, EU-standard box or pallet. Packaging can be customized to customer requirements. Environmental compliance: Our product packaging complies with Regulation (EU) 2025/40 on Packaging and Packaging Waste (PPWR), which applies directly in EU member states from 12 August 2026. |
What The Volute Is Actually Doing
Inside the casing the impeller spins and throws fluid outward. The volute collects that flow and eases it down before the discharge nozzle. That spiral wall is not decorative. It is the pressure boundary. Thin near the nose where flow first enters, thicker out where the velocity has built up. We leave extra stock on that outer wall so the machinist can clean it up on the CNC. The inlet bore has to sit dead on the impeller centerline. Off by a few thou and the seal rubs, the bearing runs hot, and the pump sounds like a tin can before the warranty is up. The discharge nozzle bolts tangent to the spiral. We check that hole pattern against your drawing on the fixture, every run.
Why A Casting Instead Of Fabricated
Some buyers ask why we do not weld plate and pipe into a housing. You can. Very small runs, maybe. But welds crack at the heat affected zone years later in corrosive service. A casting is one solid piece of 316L. No weld seam to corrode, no distortion from the welding torch, no internal vane you cannot reach to grind. 316L handles chloride water, mild process chemicals and washdown without any painted coating. It is the standard pick for seawater, utility and chemical transfer pumps for a reason.
How The Cast Runs Through Our Shop
Send us your drawing. We build the wax pattern, set it on a runner, dip the whole tree in ceramic slurry and stucco it coat after coat until the shell feels thick enough. It sits overnight to dry. Steam autoclave strips the wax out. The shell fires in the furnace, and we pour the stainless while it is still hot. Shakeout knocks the shell off. Shot blast cleans the ceramic off the as-cast skin. The rough casing goes on a pallet with its heat lot number written on the side, and it waits its turn for the CNC queue.
On The CNC Table
On the machine table, the operator faces both of the flange surfaces and bores the center passage so that it matches your impeller. The mounting holes are put in, and they are tapped according to the bolt pattern on the print. The seal seat is given a finer cut than the rest of the body. When the fixture is taken off, a dial indicator is used to swing around the flange; if it is out of flat, the part goes right back on the machine, because there is no arguing with the needle. Every cross hole is blown out before the washdown, since chips left under a bolt seat will be found later by your crew on the skid.
Before It Leaves The Shop
Every body goes on the pressure bench before packing. We pull the test up to the port pressure on your drawing and hold it on the gauge for a few minutes. Weep anywhere, back to the bench. Pass it, we wipe the surfaces, tag the heat number, wrap it for freight. Send us the drawing and your required tolerance, we quote casting plus machining together, one lead time. Buyers spec this 316L pump housing for chemical transfer, seawater service, RO skids and food processing lines where a coated steel body would not last a season.
Custom Manufacturing Process
1. Requirement Communication
We start with the drawing, the application and the order quantity. Material, dimensions, tolerances, operating conditions and any packing or documentation requirement are recorded before quoting.
2. Technical Evaluation
The engineering team reviews wall sections, machining stock, casting feasibility and the critical fits. If a feature is difficult to cast or machine, it is raised before tooling begins.
3. Process and Sample Confirmation
The process route is fixed, and a sample is made when the project requires one. The sample is checked against the drawing and confirmed before the mass production.
4. Mass Production
Production is scheduled against the confirmed specification and order quantity. Progress is tracked through casting, machining and finishing.
5. Quality Inspection
Dimensional and visual checks are carried out according to the agreed requirements. Inspection records are kept with the batch.
6. Packaging and Delivery
The finished parts are packed for export, labelled as agreed, and prepared for the shipment with the required documents.
The pump volute casing is machined with the pump body, and the pump housing is checked on the same fixture.
Company Profile & FAQ
| At a Glance | |||
| Founded | 2010 | ||
| Factory Area | About 60,000 m² in Kazuo County, Liaoning | ||
| Staff | Around 120 people, including engineers and QC | ||
| Experience | 16 years of silica sol investment casting | ||
| Export Markets | Japan, South Korea, Europe and North America | ||
| Capacity | 1,000 tons per year of precision castings | ||
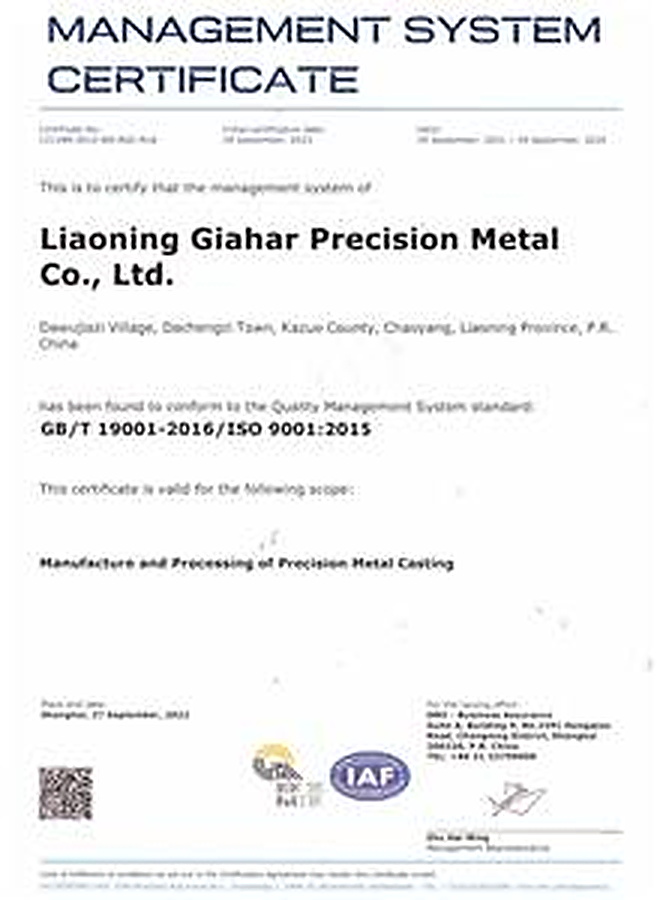
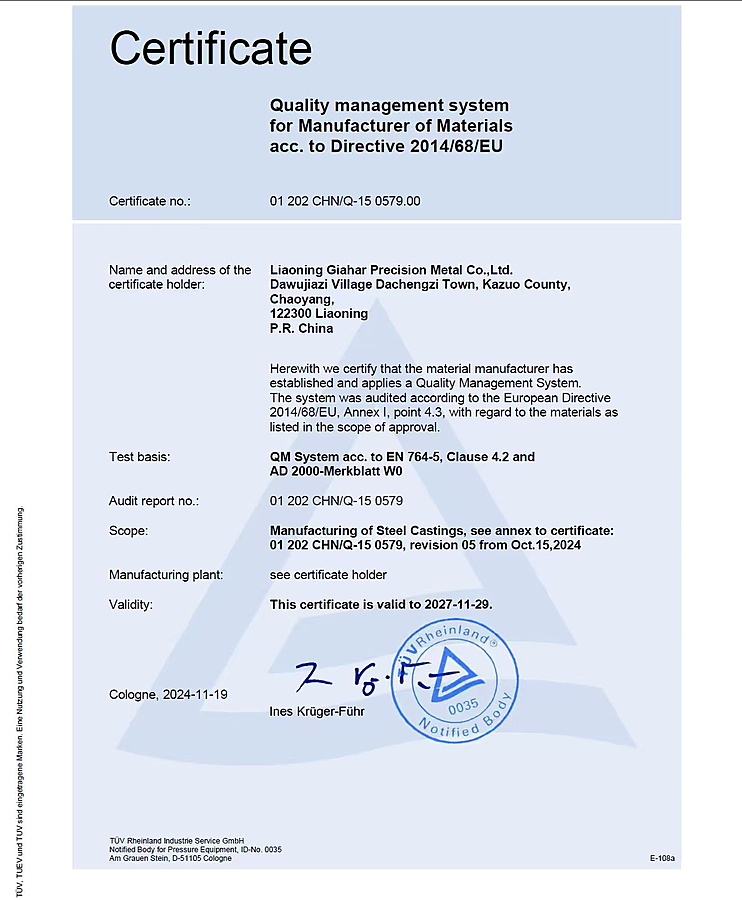
| Certifications | DNV ISO 9001 Quality Management System Certificate; TUV PED 2014/68/EU Pressure Equipment Certificate
| ||
| FAQ | |||
| Q: Can you produce parts from my drawing or sample? | |||
| Yes. Send a 2D drawing, a 3D model or a physical sample. Our engineer will review the wall sections, tolerances and machining stock before quoting. Any risk is raised before the sample stage. | |||
| Q: Do you provide material certificates and inspection reports? | |||
| Mill certificates to EN 10204 3.1, heat treatment records and dimensional reports can be supplied. PED 2014/68/EU documentation and a hazardous-substance-free declaration covering RoHS and REACH are also available. The required document package is confirmed at quotation. | |||
| Q: Can you do machining, heat treatment and surface finishing in-house? | |||
| Yes. The castings are moved from our foundry to our CNC shop. Stress relief is carried out after the casting, and solution annealing can be done in our controlled furnace when the material specification requires it. Passivation and pickling are also handled on site. Since the same team controls casting, heat treatment and finishing, the parts do not have to travel between different vendors, which reduces the handling damage and keeps the production route short. | |||
| Q: Which standards do you work to? | |||
| European work generally follows ISO. Customer-specific standards are reviewed against the drawing, and the inspection standard is confirmed before the order is released. | |||
| Q: What are the MOQ and lead times? | |||
| MOQ is normally 100–500 pcs for new tooling, and for repeat orders the quantity can be lower. New product development takes about 2 months, while the precision casting production takes about 1.5 months. The final schedule is confirmed against the drawing, the order quantity and the current production load. | |||
Pump Body FAQ
| Product-Specific FAQ | |
| Q: What material is used for the pump body? | |
| 316L stainless steel is the standard grade. It is used for chemical transfer, seawater and washdown duties where cast iron would corrode. | |
| Q: Is the pump body pressure tested? | |
| Yes. The body is put on the pressure bench before packing, and the test pressure is taken from the drawing. A body that weeps is returned to the bench. | |
| Q: Can you machine the flange and seal seat to my drawing? | |
| Yes. The flange faces, bore and seal seat are machined to the drawing. A first-off part is checked before serial production. | |
| Q: Can you supply a replacement for an existing pump? | |
| Yes. Send the drawing, the pump model or a worn body. We check the flange pattern, the bore and the seal seat before the quotation, and if something does not match, we will tell you before the order is placed. |